
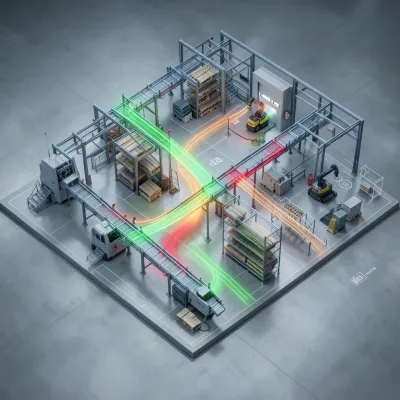
The following is an excerpt from “Plant Layout and Flow: Designing Efficient Factory Floors for Throughput” by Jean Hawkins, available on MixCache.com.
Introduction
Factories are built to move value. The faster and more smoothly material flows from receipt to shipment, the more throughput you create with the same people, space, and capital. Yet many plants still operate with legacy “spoke-and-hub” departments, long walks, and invisible queues that hide delays. This book is about turning that complexity into clarity—using layout and flow design to convert wasted motion and waiting into productive work.
Our approach blends industrial engineering fundamentals with proven shop‑floor practices. You will see how Little’s Law links work‑in‑process, lead time, and throughput; how bottlenecks dictate output; and how variability amplifies queues. We translate those principles into tangible design choices: U‑shaped lines that shorten travel and enable one‑piece flow, cellular manufacturing that pulls formerly scattered operations into tight workcells, and mixed‑model lines that meet demand without ballooning inventory. Throughout, the emphasis is on pragmatic tools you can apply immediately.
Designing a great layout is not an abstract exercise. It starts with a clear view of the current state—value stream maps that expose delays, spaghetti diagrams that reveal motion waste, and time–motion studies that quantify work content. From there, we build concept alternatives using block layouts and from‑to charts, then evaluate options with material handling strategies, aisle sizing, storage policies, and support‑area placement. You will learn when to choose gravity flow racks over powered conveyors, when AGVs outperform tugger loops, and how kitting can relieve line congestion.
Because decisions are only as good as the risks you’ve surfaced, we devote significant attention to validation. Discrete‑event simulation and digital twins help you test staffing levels, buffer sizing, changeover policies, and dispatching rules before concrete is poured. We connect models to real data—cycle times, demand mixes, arrival variability—so you can see how a proposed layout performs on its worst day, not just its average one. The result is confidence in throughput, lead time, and space claims.
A layout that performs on day one must also improve on day one hundred. That is why this book integrates 5S, visual management, standard work, and quick changeover (SMED) into the physical design. We frame pull systems—kanban, supermarkets, and replenishment routes—as part of the architecture, not bolt‑ons. Ergonomics, quality at the source via poka‑yoke, and maintenance access are treated as core flow enablers, ensuring safety and quality rise with productivity instead of trading against it.
Finally, flow must make financial sense. We connect design choices to capacity, labor productivity, footprint, and total cost to serve. You will learn how to compare alternatives on CapEx and ongoing operating expense, how to phase implementations without stopping the plant, and how to track benefits using throughput, lead time, and inventory turns. Case studies from discrete assembly, fabricated metals, and consumer goods illustrate the path from concept to cutover.
Whether you are a manufacturing engineer redesigning a line, a plant manager expanding a facility, or a lean practitioner targeting bottlenecks, this book equips you with a complete toolkit. By combining industrial engineering principles with real‑world layouts—and by validating designs with simulation and continuous improvement—you will be able to design efficient factory floors that maximize flow, minimize waste, and deliver predictable throughput.
Read “Plant Layout and Flow: Designing Efficient Factory Floors for Throughput” on MixCache.com →
Please log in or create an account to leave a comment.
No comments yet. Be the first to say something.